Best Roto Moulding Machine Choices for Durable Plastic Production
2026-09-14
When it comes to producing plastics that can shrug off years of rough handling, the choice of roto moulding machine isn't just a technical detail—it's the quiet engine behind every durable tank, sturdy playground slide, and rugged industrial bin. Yet with a flood of options on the market, finding a machine that balances precision, longevity, and real-world throughput often feels like guessing in the dark. Enter Rising Sun, a name that keeps surfacing in conversations among plant managers who refuse to trade build quality for speed. In this guide, we skip the glossy brochures and dig into what actually separates a workhorse from a garage queen, so you can make a choice that doesn't just survive your production schedule—it thrives in it.
What Separates Long-Lasting Rotomolded Parts from the Rest?
The real difference starts long before the mold closes. Long-lasting rotomolded parts use virgin polyethylene grades that retain impact strength even after years of UV exposure and freeze-thaw cycles. Cheap regrind or blended resins might save a few dollars upfront, but they turn brittle after a couple of seasons outdoors. You can spot the better material by the way the part feels—it has a slight give, not a hard, glassy surface that signals over-baked plastic.
A consistent wall is the unsung hero. In rotomolding, the plastic doesn't flow under pressure; it tucks into corners by gravity and rotation. That means sharp internal corners and abrupt thickness changes become hidden failure points. Long-lasting designs smooth out those transitions, add generous radii, and often include molded-in ribs that do double duty—stiffening the part without creating thick, sink-prone sections. You can tell a part that will crack by year three just by looking at the inside radius: if it's sharp, stress will concentrate there no matter how good the resin is.
How the part cools is just as critical as how it's heated. Slow, controlled rotation during cooling prevents warping and locked-in stress that later shows up as a split seam. The best shops also trim and finish parts after they've fully stabilized, not while still soft from the oven. It's the kind of patience you won't see in a spec sheet, but it's exactly what separates a kayak that survives a decade of river rocks from one that cracks on its third launch.
Picking a Machine That Handles Thick-Wall Molding Without Fail
Thick-wall parts live and die by cooling time, so the machine's real job goes far beyond just filling the cavity. Look for a press with robust platen parallelism and enough clamp tonnage to resist core deflection over the long hold phase, but don't stop there. The injection unit needs to hold pressure steadily for minutes, not seconds, without drifting. A machine with weak hydraulic or servo response will cause sink marks and voids you can't fix later. Check the manufacturer's data for pressure repeatability at low flow rates, not just peak numbers.
Screw geometry matters more than most buyers realize. Thick sections demand a gentle melt with minimal shear heating, otherwise you degrade the polymer and build in residual stress. A low-compression screw with a longer feed zone and a deeper metering channel lets you run a lower barrel temperature while still getting a homogenous melt. Avoid machines optimized for thin-wall, high-speed filling—they overwork the resin. If the supplier can't tell you the screw's compression ratio and L/D for your specific material, walk away.
Finally, consider the mold open/close system. Thick-wall molds are often heavy and may have deep cores or side actions that need slow, controlled movement. A machine with linear guide rails on the moving platen and a low-pressure mold protection feature will save you from cracked inserts and premature wear. Ask for a demo with a heavy tool, not an empty clamp, and watch how smoothly it transitions from fast approach to final lock-up. The best machine for thick-wall work feels deliberate, not twitchy.
Energy Use and Cycle Times: The Real Cost Drivers in Rotational Molding
In rotational molding, the furnace isn't the only place where money quietly leaks away. Cycle time often dictates energy consumption more directly than oven temperature settings alone. A mold that lingers in the heating phase—even by a few minutes—forces the burners to work longer, and those extra minutes compound across every part produced. The real cost driver isn't just the price per kilowatt-hour; it's the total time the mold spends absorbing heat while the machine stays idle in other stages.
Cooling time is equally deceptive. Water sprays and forced air might seem cheap compared to gas, but a poorly designed cooling sequence extends the overall cycle and ties up the mold, reducing daily throughput. Operators who chase faster heating without rethinking mold release or part wall thickness often end up with warpage, which leads to scrap—and scrap carries its own hidden energy bill. Every rejected part represents the full energy investment of a previous cycle, wasted.
Trimming cycle time isn't about rushing the process; it's about eliminating idle minutes. Simple changes—like preheating the mold between cycles, adjusting rotation ratios to improve heat transfer, or using thinner mold shells with better conductivity—can drop energy use by 10–15% without touching the oven's temperature dial. The most profitable molds aren't the ones that heat fastest; they're the ones that spend the least total time from powder to finished part.
Material Compatibility: Why Not Every Polymer Works in Every Machine
A polymer's melting point alone never tells the full story. Even if a machine can reach the required temperature, the way a material flows under pressure, how it responds to shear inside a barrel, and whether it releases corrosive byproducts can make the same setup a dream for one resin and a maintenance nightmare for another. PVC, for instance, degrades rapidly when held at processing heat in standard steel barrels, releasing hydrochloric acid that eats away at screw surfaces unless expensive nickel-plated alloys are used. Meanwhile, a simple polypropylene part can be churned out on almost any basic single-screw extruder without a second thought.
Thermal stability windows are just as critical as peak temperatures. Some engineering polymers like PEEK or PPS require sustained barrel temperatures above 350°C, which many commodity-grade machines simply can't maintain without burning out heater bands or softening their own structural components. On the flip side, heat-sensitive materials such as EVA or certain TPUs will crosslink or char if they linger too long in a hot runner system designed for faster-cycling polyolefins. It's not about the machine being "bad"—it's about the residence time, screw geometry, and temperature control range being tuned for a completely different viscosity profile.
Additives and fillers introduce another layer of mismatch. Glass-fiber-reinforced nylon will chew through a standard nitrided screw and barrel in weeks, whereas unfilled nylon would run for years on the same equipment. Abrasive wear isn't the only concern: some flame-retardant packages plate out on die lips, conductive carbon black alters melt viscosity unpredictably, and hygroscopic resins like PET or polycarbonate demand vented barrels or aggressive drying that many machines never accounted for at the design stage. Choosing a polymer without checking how it interacts with every wetted surface—from feed throat to nozzle tip—is a shortcut to scrapped batches and premature hardware replacement.
From Kayaks to Chemical Tanks: Matching Machine Size to Product Demand
Rotational molding shops often juggle a wild range of part sizes—one day it's a sleek kayak hull, the next a bulky chemical storage tank. That spread isn't just a scheduling headache; it dictates the machine envelope. A small shuttle machine with a 60-inch swing might handle a kayak comfortably, but try loading a 5,000-gallon tank into that same oven and you'll quickly find the door opening, offset arm length, and interior clearance all working against you.
Matching machine size to product demand starts with honest part measurements, not guesses. The largest diagonal dimension of the mold—plus room for the arm swing and any external fixtures—sets the minimum oven diameter and depth. Overlooking that math leads to scraped molds, uneven wall thickness, or worse, a mold that simply won't fit. Conversely, running small parts on a massive machine wastes energy and cycle time, since you're heating and cooling far more steel than necessary.
The smart approach is to map your actual product mix before buying or upgrading. If 80% of your work sits in the kayak-to-small-tank range, a mid-size carousel or independent-arm machine with adjustable stations might beat a giant fixed oven. But if you regularly produce industrial tanks over 3,000 gallons, you'll need that bigger swing, taller ceiling, and heavier load capacity from day one. It's less about having the biggest machine and more about having the right clearance, swing, and thermal control for the parts you actually run.
Five Signs Your Roto Moulding Machine Is Built for Continuous Duty
Continuous duty isn't something a manufacturer stamps on a spec sheet for fun. It shows up in the details that get stressed after the warranty period ends. Look past the horsepower figures and pay attention to how the frame is put together. A machine built to run around the clock typically carries a fully welded base, thicker corner gussets, and bearing housings that are machined after welding rather than bolted on as an afterthought. Those choices are less about saving money and more about stopping hairline cracks before they start.
Then there's the cooling system. Plenty of rotomoulders learn the hard way that a machine can handle heat, but it's the repeated thermal cycling that kills components. Continuous-duty designs often route cooling air through dedicated channels instead of relying on ambient airflow. You might notice larger diameter fans, copper or aluminium heat exchangers, and temperature sensors placed at the mould spindle rather than the oven wall. That sensor position matters because it tells you what the tooling actually feels, not what the heater box thinks it's doing.
Drive components are another giveaway. If you spot chain tensioners that are spring-loaded rather than fixed, or gearboxes with oil sight glasses and external cooling fins, that's usually a sign the builder expected the machine to run shift after shift. The same goes for electrical panels: continuous-duty rotomoulders tend to have contactors and relays rated for more cycles than you'd need in a short-run shop, plus terminal blocks that are labelled and spaced for easy troubleshooting at 2 a.m. It's not glamorous, but those small choices are what keep the line moving when the order book is full.
FAQ
The key lies in even heat distribution and stable arm rotation. A quality machine uses precise temperature control and a balanced arm system to avoid thin or thick spots. Seal and bearing materials also matter because they determine whether consistency holds up after months of continuous running.
Multi-arm machines let you run different molds at the same time, which shortens cycle times without sacrificing wall uniformity. However, they demand more careful programming—otherwise parts on different arms can end up with slight density differences.
LLDPE is the go-to for most durable containers because it resists impact and flows well. Cross-linked polyethylene (XLPE) suits parts that need chemical resistance and higher heat tolerance. Nylon is sometimes blended in to add stiffness.
Cooling too fast can introduce internal stress, leading to warpage or micro-cracks. A staged approach works better—let heat dissipate naturally first, then apply forced air so the polymer crystallizes more fully.
They can be, but you need to inspect the main shaft bearings, arm wear, and heating system history. A second-hand machine without complete service records often hides uneven heating problems that will eventually hurt your yield rate.
Open-flame heating is faster but creates more hot spots, which works for thick-walled simple shapes. Convection heating spreads warmth more evenly, so complex or thin-walled durable parts benefit, though cycles tend to run slightly longer.
Check arm bolts and bearing clearance every week, and clean burners or heating elements monthly. Don't ignore seal strips and thermocouple calibration—temperature drift can directly alter product density and wall thickness.
For hollow, seamless, impact-resistant parts, roto moulding has a clear edge. But wall thickness tolerances and cycle times are not as tight as injection moulding, so the choice depends on the exact geometry and production volume.
Conclusion
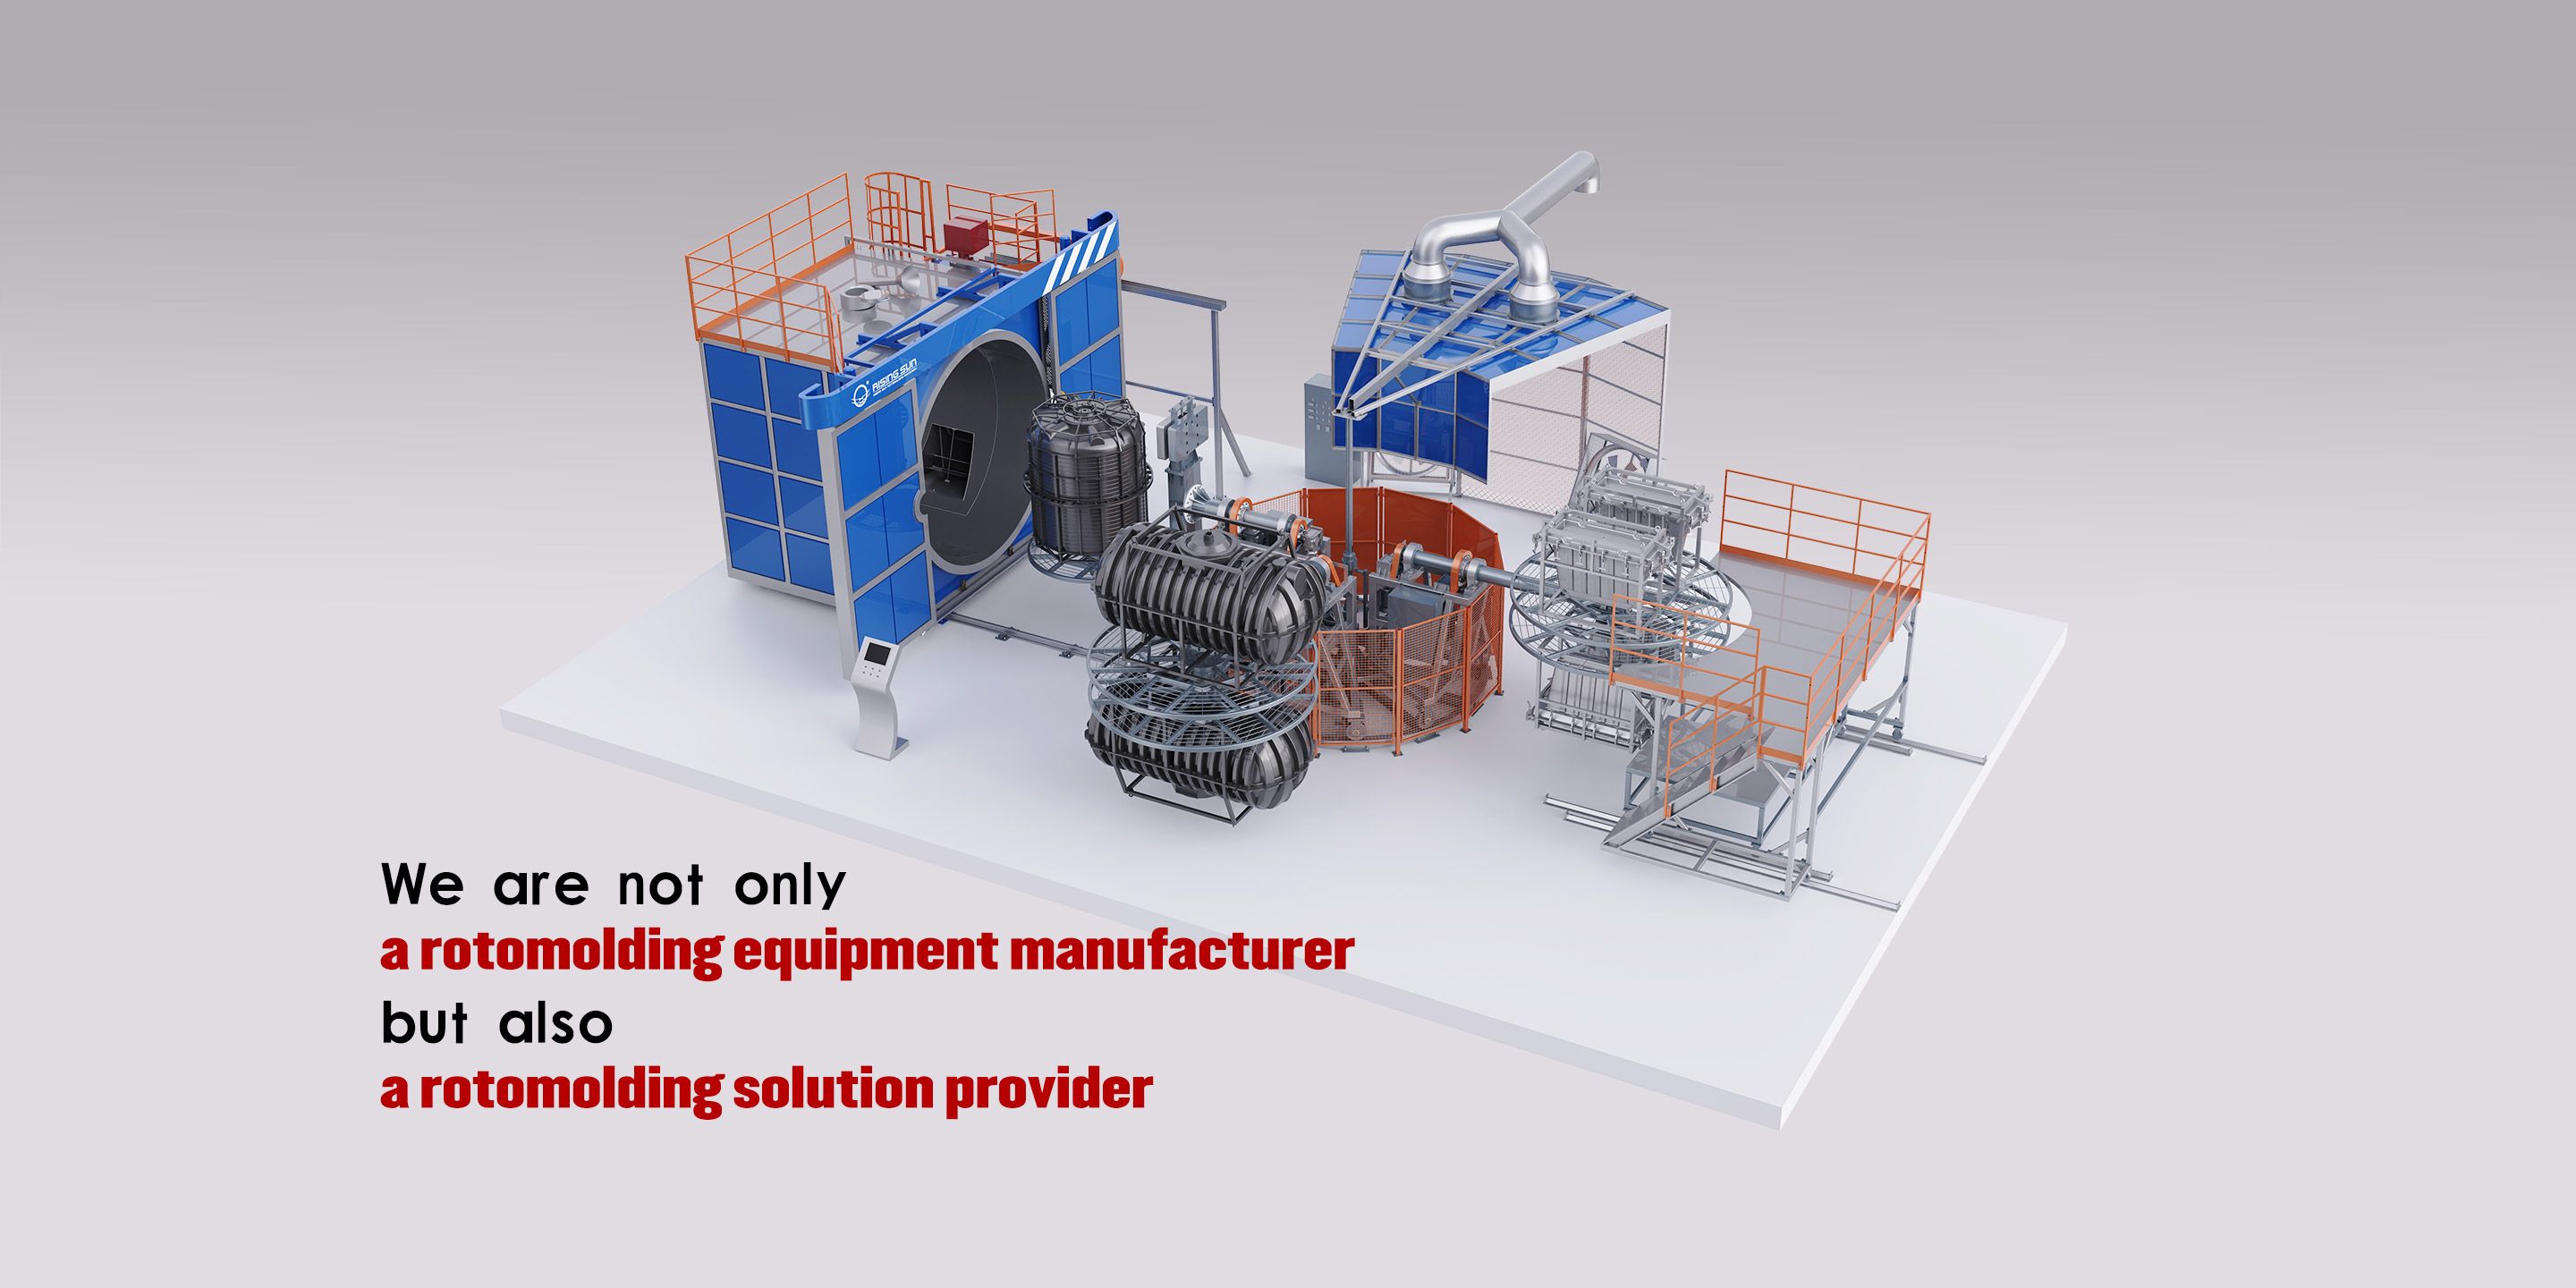
The real difference between rotomolded parts that survive years of abuse and those that crack or warp comes down to how evenly a machine distributes heat and material across the mold. A quality roto moulding machine doesn't just spin the mold; it manages oven temperatures in zones, allows precise control of the heating and cooling cycle, and keeps the mold moving on both axes without dead spots. This is especially critical for thick-wall products like large tanks or heavy-duty playground components, where an underheated core or an overheated skin can ruin the entire batch. When comparing machines, look for models with adjustable arm speeds, reversible rotation, and enough torque to handle heavy molds without stalling. Material behavior matters too: polyethylene and nylon have very different melting and cooling characteristics, so a machine that gives you fine temperature ramps and independent oven controls will handle a broader range of polymers without scorching or incomplete fusion.
Beyond the molding itself, the numbers that hit your bottom line are energy consumption and cycle time. A well-insulated oven with efficient burners or electric heating elements can cut fuel costs noticeably, while a properly sized cooling fan or water mist system shortens the time before demolding without shocking the part. Machine size should match the products you actually run; a small kayak mold doesn't need a 4-meter swing, but a chemical tank does, and oversized machines waste energy on every cycle. For continuous-duty shops, look for signs of industrial build: heavy-duty sealed bearings on the arm, a rigid frame that won't twist under load, easily cleanable oven floors for polymer drips, and a control system that logs cycle data for repeatability. If the machine struggles to maintain temperature during back-to-back runs or the arm flexes when a full mold is mounted, it will fail long before your production schedule does.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com
